이 글은 CMS에서 편집할 수 있도록 준비되어 있습니다. 최종 콘텐츠는 섹션별로 입력하고 관리할 수 있습니다.
01What machine tending automation actually does
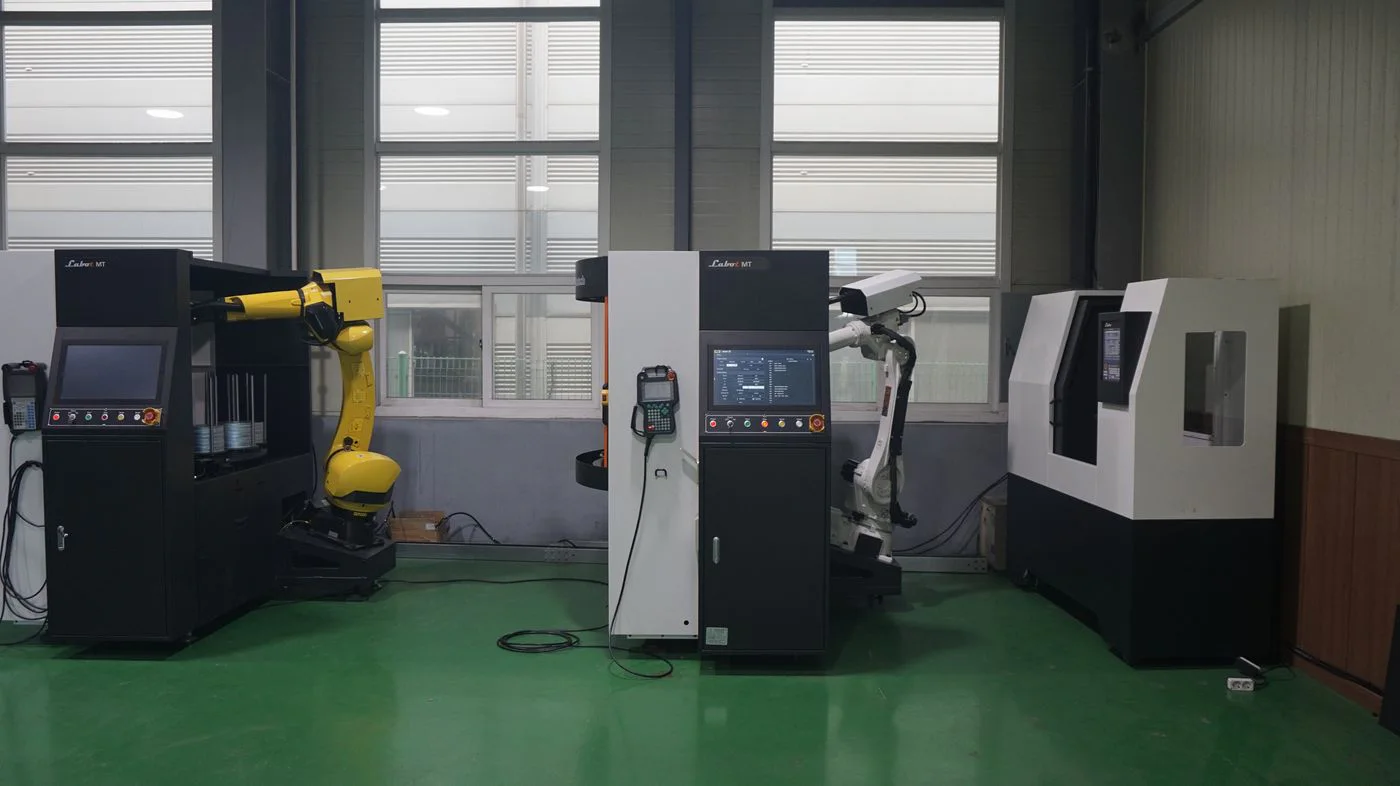
Machine tending is the act of loading a raw part into a CNC machine, starting the cycle, and removing the finished part. It is repetitive, physically demanding, and a major reason spindles sit idle in an otherwise busy shop. A robotic machine tending system automates that loop. Parts are organized in a tray, drawer, or turntable. A robot picks each one, loads it, waits out the machining cycle, unloads it, and moves on. Done well, the cell runs through breaks, shift changes, and overnight without an operator standing in front of it. The goal is not to remove people from the shop. It is to stop paying skilled machinists to open and close a door.
02When a shop is ready to automate
Automation does not require high volume. It requires repeatability. If you run the same part family often enough that setup time is amortized, you are a candidate, even at a few hundred pieces per run.
- You have a repeatable part family. Similar geometry, similar fixturing, similar cycle time.
- Your cycle time is long enough to be worth waiting out. Roughly 90 seconds and up is where unattended running starts paying for itself.
- You are turning away work or running overtime. Capacity, not headcount, is the constraint.
- Your operators are doing more valuable work elsewhere: inspection, setup, programming, deburring.
03Choosing a loading method
The loading method is the single biggest decision in a tending project, and it is driven by your part size, floor space, and how long you want the cell to run unattended.
Trays and drawers
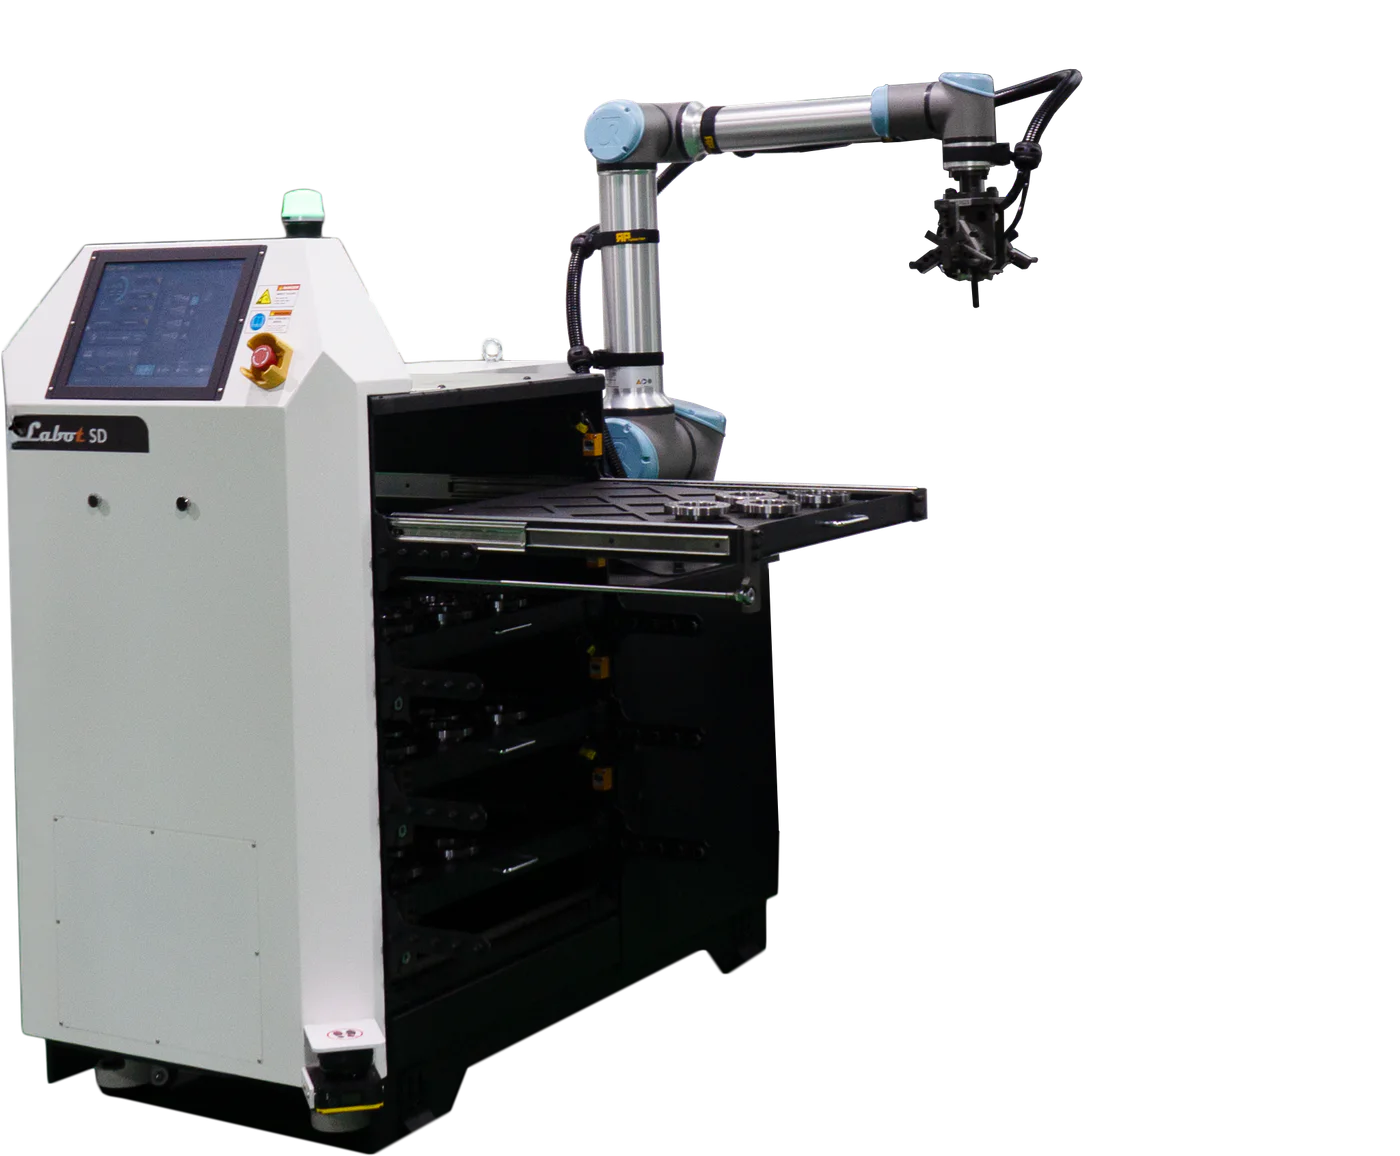
Honeycomb stacking trays hold the most parts in the least floor space. Drawer-based systems let an operator reload from outside the cell while the robot keeps working inside it.
Turntables
A split turntable loads and unloads simultaneously. The operator fills one side while the robot works the other, removing the reload pause from the cycle.
Carts
Cart-based handling decouples part staging from the cell. Load a cart at a bench, roll it in, and roll the empty one out.
04Integrating with your existing CNCs
The most common objection to tending automation is that it will not talk to the machines already on the floor. In practice, integration comes down to what signals the control exposes and what protocol it speaks.
- Ethernet-based controls are the easiest path. Cycle start, door, chuck, and alarm states are read directly.
- Discrete I/O covers everything else. Relay-level connections handle machines without network access.
- Mixed fleets are normal. A single cell can be configured against different machine brands.
- On-site commissioning verifies behavior. Signal timing is confirmed per install, not assumed from a datasheet.
05What setup looks like in practice
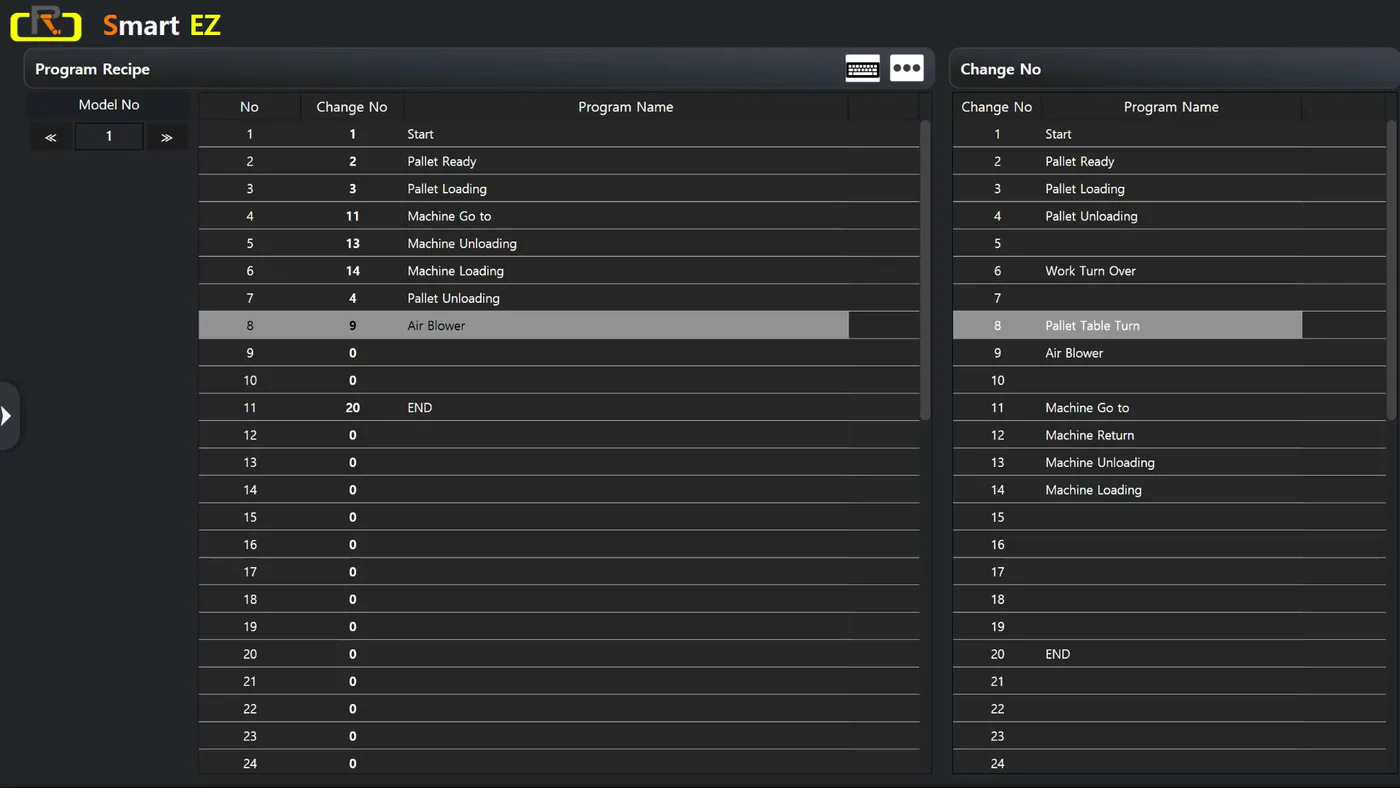
On a modern tending platform, the operator never touches robot code. Setup is a guided sequence in the control software: pick the model, pick the pallet type, teach the workpiece position, save the recipe, and apply it to the machine. The practical consequence is that changeover becomes a recall, not a reprogram. A part you ran last month is a saved recipe, and the second run costs minutes instead of hours.
06Building the business case
Skip the generic ROI calculator. The numbers that matter are specific to your floor, and there are only four of them.
- Additional spindle hours per week. Unattended run time you do not have today.
- Labor reallocated, not eliminated. What that machinist does instead, valued honestly.
- Scrap and rework reduction. Consistent loading removes a class of human error.
- Capacity you can now quote. The work you turn away today because the machines are full.